Candy Machine Manufacturers serve very different production needs. Some build compact equipment for small-batch kitchens. Others engineer high-speed lines for large confectionery plants. The distinction matters. A machine suited to chocolate may not handle gummy depositing or hard-candy forming with the same consistency.
Confectionery scientist Richard W. Hartel has published extensively on confectionery processing. The following is an editorial paraphrase of the practical perspective his work supports, not a verified verbatim quotation: “Choose equipment by the product and process it must control, not by output claims alone.” That is a useful test. A chocolate tempering system manages temperature and crystal formation. A gummy line must control depositing, cooling, and release. A hard-candy cooker needs accurate heat management. Small details show up in the finished batch.
This guide introduces the main types of Candy Machine Manufacturers, from specialists in single machines to suppliers of integrated production lines. It also considers custom builders and manufacturers focused on particular products, such as chocolate, gummies, or hard candy. Buyers should compare sanitation access, changeover time, production capacity, and technical support—not just the brochure figures. Ask to see the equipment run with a comparable product. Watch the feed, the controls, and the finished pieces. A neat sample is not the whole story. Even experienced buyers can overlook maintenance access; that deserves a second look. Which manufacturer fits best depends on the recipe, available space, staff skills, and planned growth.
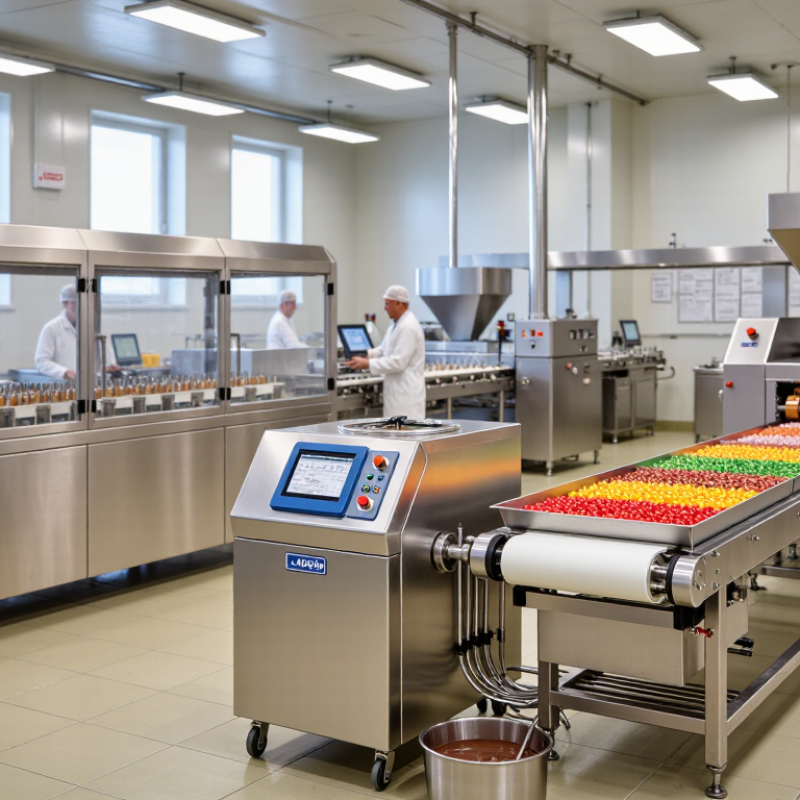
Batch-cooker manufacturers build equipment for heating candy syrup in controlled lots. For hard-crack candy, the finished syrup commonly reaches 149–154°C. At this stage, little water remains, and a cooled drop sets into a brittle, glass-like piece. It should snap cleanly, not bend. That is the target.
A cooker’s heating surface, batch size, and agitation all affect how evenly the syrup warms. Operators often watch a calibrated thermometer and check the syrup’s appearance near the endpoint. A few degrees matter. A probe touching the vessel wall may read hotter than the syrup itself, so its position deserves attention. Humidity and ingredient ratios can also shift the result; the temperature range is a useful guide, not a promise for every formula.
Manufacturers may offer jacketed kettles, controlled heating, scrapers, and discharge systems to help manage thick, hot syrup. These features can reduce scorching and make batches easier to transfer, but they do not replace careful testing. Hot syrup is unforgiving. Even experienced teams can overshoot the endpoint while moving slowly from heating to discharge. That part is easy to underestimate. A small trial batch can reveal whether the cooker’s heat response suits the recipe before production scales up.
Depositing-machine manufacturers build systems that meter liquid or semi-liquid candy into molds. The best match depends on shape, viscosity, and target weight. For round gummies, a multi-nozzle depositor can fill several cavities evenly. For layered chews or filled centers, controlled timing matters more than speed. A narrow nozzle helps form small details, but thicker mixtures may need wider openings to prevent inconsistent flow. Tiny differences show up fast.
Product demand also makes repeatable portioning important. The National Confectioners Association’s 2024 State of Treating report says 98% of Americans enjoy chocolate or candy. That broad appeal does not mean one machine suits every product. Ask manufacturers for trial runs using your actual recipe, mold, and target piece weight. Review fill accuracy, changeover time, and cleaning access—not just rated output. A glossy sample can hide uneven centers.
Tips: Bring a real batch of your mixture to the factory test. Check the first and last pieces from each run. Record weight variation and inspect corners for trapped air. Depositors can struggle when temperature shifts alter viscosity; this is easy to overlook. Keep a little room in the specification for real production conditions.
A qualitative guide to how common depositing-machine configurations align with candy formats.
Scores indicate relative process fit, not measured machine performance. Actual suitability depends on recipe, viscosity, product dimensions, and equipment design.
For extrusion and forming equipment, kg/h is useful only when test conditions match your candy. An extruder’s output changes with rope diameter, recipe viscosity, and cutting speed. Forming machines may handle different rates depending on cavity size, mold layout, and product release. A supplier’s maximum figure is not always a realistic shift target. That gap matters.
Compare machines using the same product weight, shape, and operating period. Ask for net saleable kilograms per hour, not just material fed into the line. Request a continuous production trial and record stops, rejects, and changeover time. A line rated at 300 kg/h may deliver less after cleaning or mold adjustments. Specifications can look clean; production rarely is. I would also check whether the quoted capacity includes cooling and downstream handling, since a fast former can still feed a slower cooling tunnel. Keep a sample from the trial and weigh it against the recorded output. Small details can expose an optimistic estimate.
| Manufacturer Type | Typical Process | Common Candy Products | Indicative Capacity (kg/h) | Key Capacity Factors |
|---|---|---|---|---|
| Rope extrusion and sizing equipment manufacturers | Cooked candy mass is formed into a continuous rope, then sized and cut or sent to downstream forming equipment. | Hard candies, chewy candies, filled candy ropes | 100–600 | Rope diameter, number of lanes, recipe viscosity, cooling time, and the speed of downstream cutting or wrapping equipment. |
| Hard candy stamping and forming equipment manufacturers | Conditioned candy ropes or batches are portioned and shaped by rotary or die-forming systems. | Boiled sweets, lozenges, filled hard candies | 100–500 | Piece weight, die layout, forming speed, product temperature, and whether the line handles filled or unfilled pieces. |
| Depositing and moulding equipment manufacturers | Cooked candy mass is deposited into reusable moulds and cooled or set before demoulding. | Gummies, jellies, fondants, deposited hard candies | 100–1,000 | Depositor head configuration, mould count, deposit weight, setting time, and the cooling or conditioning system. |
| Starch-moulding line manufacturers | Product is deposited into impressions made in starch trays, then conditioned, removed, and finished. | Gummies, jellies, starch-moulded creams | 100–1,000 | Tray dimensions, moulding and depositing rates, drying or setting time, product size, and line automation. |
| Licorice and aerated candy extrusion equipment manufacturers | Prepared candy mass is extruded through a die and cut or shaped into finished pieces. | Licorice twists, ropes, bars, aerated candy pieces | 100–600 | Die size and shape, mass temperature, product density, cutting method, and the number of extrusion lanes. |
| Chewing gum and bubble gum extrusion equipment manufacturers | Gum mass is mixed, extruded into a rope or sheet, and then sized, cut, or formed. | Chewing gum sticks, pellets, bubble gum pieces | 50–500 | Gum formulation, extrusion temperature, product format, cooling requirements, and downstream sizing capacity. |
Note: Capacity figures are indicative ranges for industrial equipment, not guaranteed output specifications. Actual throughput depends on the product recipe, piece size, operating conditions, line configuration, and the capacity of connected equipment.
Candy machine manufacturers often specialize in cooking, forming, cooling, or packaging. For finished sweets, packaging-machine manufacturers help connect production output with reliable wrapping and handling. The right line speed is not simply the fastest number on a brochure. It must suit the candy’s size, shape, temperature, and tendency to stick or break.
A practical assessment starts with actual output per minute, not the machine’s maximum rated speed. A line producing 300 pieces per minute may need a wrapper that handles more than 300, allowing for brief stops and uneven feeding. Small details matter. Check whether the infeed can orient mixed-shaped pieces, and whether film changes or jam clearing interrupt production. Ask for a test using representative product, packaging material, and operating conditions. Watch for crushed corners, loose seals, and sweets arriving in clusters. These observations reveal more than a short demonstration at peak speed.
Also consider changeovers. A manufacturer should explain adjustment time, cleaning access, spare-part availability, and how speed is verified during routine production. Faster equipment can create bottlenecks if upstream cooling or product handling cannot keep pace. One assumption deserves a second look: a single speed target may not fit every candy variety. Record results across several runs, then choose a line speed the team can sustain—not merely reach once.
Turnkey-line manufacturers supply connected systems for cooking, depositing, cooling, coating, and packaging candy. Their value is not just speed. A line must be designed for practical cleaning, with accessible product zones, suitable food-contact materials, and clear equipment documentation. FDA 21 CFR Part 117 sets cGMP requirements for covered food facilities; it does not make every equipment supplier responsible for a candy plant’s food-safety plan. The facility remains accountable. Details matter.
FDA’s 2015 economic analysis for the Preventive Controls for Human Food rule estimated that about 73,000 facilities could be covered. That scale makes equipment choices consequential: poorly drained surfaces or hard-to-reach guards can complicate sanitation records and inspections. A capable turnkey supplier should provide material specifications, cleaning guidance, and support for hazard-analysis discussions, while leaving final controls to the food operator. Ask how the line handles allergen changeovers, washdown, and product buildup around depositor nozzles. These answers should be specific, not sales language. Even a well-built line can leave gaps; factory trials and site acceptance checks deserve careful review.
Same Day Shipping
ISO Certified Production